| Industry | Aggregate & bulk material handling |
|---|---|
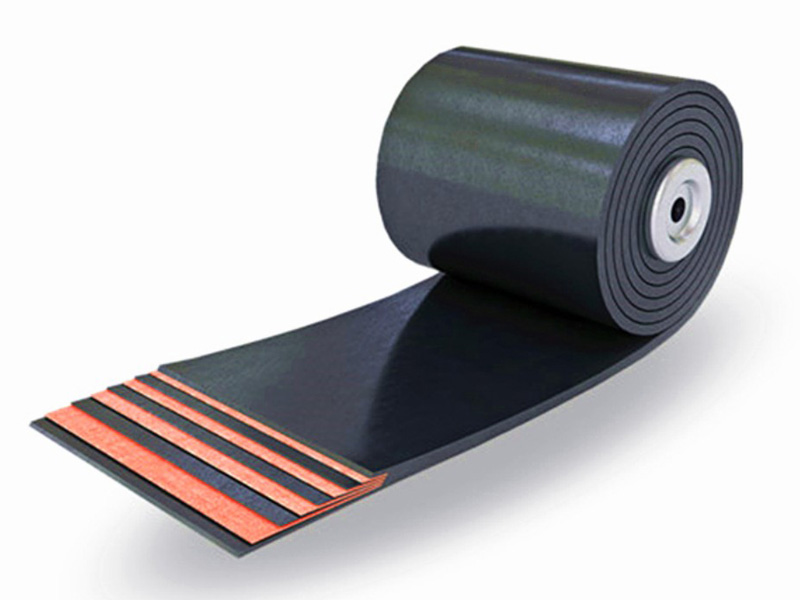
| Belt supplied | EP / NN Fabric Core Belt |
| Scope | Belt selection, compounding, supply and technical support |
Project Background
A sand and aggregate quarry produces crushed stone, manufactured sand and gravel for concrete and road construction. The conveyor system transports crushed rock from primary crusher to screening plant and stockpiles. Material includes sharp angular crushed stone up to 120 mm, high hourly throughput. Drop height at feeding chute creates heavy impact. Ordinary belts were easily cut, gouged and worn through quickly.
Challenges
- Sharp crushed stone causes cutting, gouging and heavy abrasion
- High impact at transfer points from falling rock
- Outdoor site with sun exposure, rain and frost
- High production volume requires long belt life to avoid production halt.
Solution
High abrasion & impact resistant multi-ply EP rubber conveyor belts with extra thick top cover. Impact beds are installed at loading zones. Belt cleaners and side sealing skirts reduce sand and stone spillage.
Application Result
Belt service life increased from 4–5 months to 20 months. Belt puncture and cutting failures reduced obviously. Stable transportation of aggregates improved overall crushing plant uptime. The quarry cut belt procurement and repair costs substantially.
Do you want me to shorten these 4 cases into concise versions suitable for Google product description?
Have a Similar Application?
Every site is different — material, lump size, drop height, temperature and duty cycle all change the belt specification. Send us your working conditions and we will recommend the carcass, cover grade and cover thickness, with budget pricing.
Discuss My Application