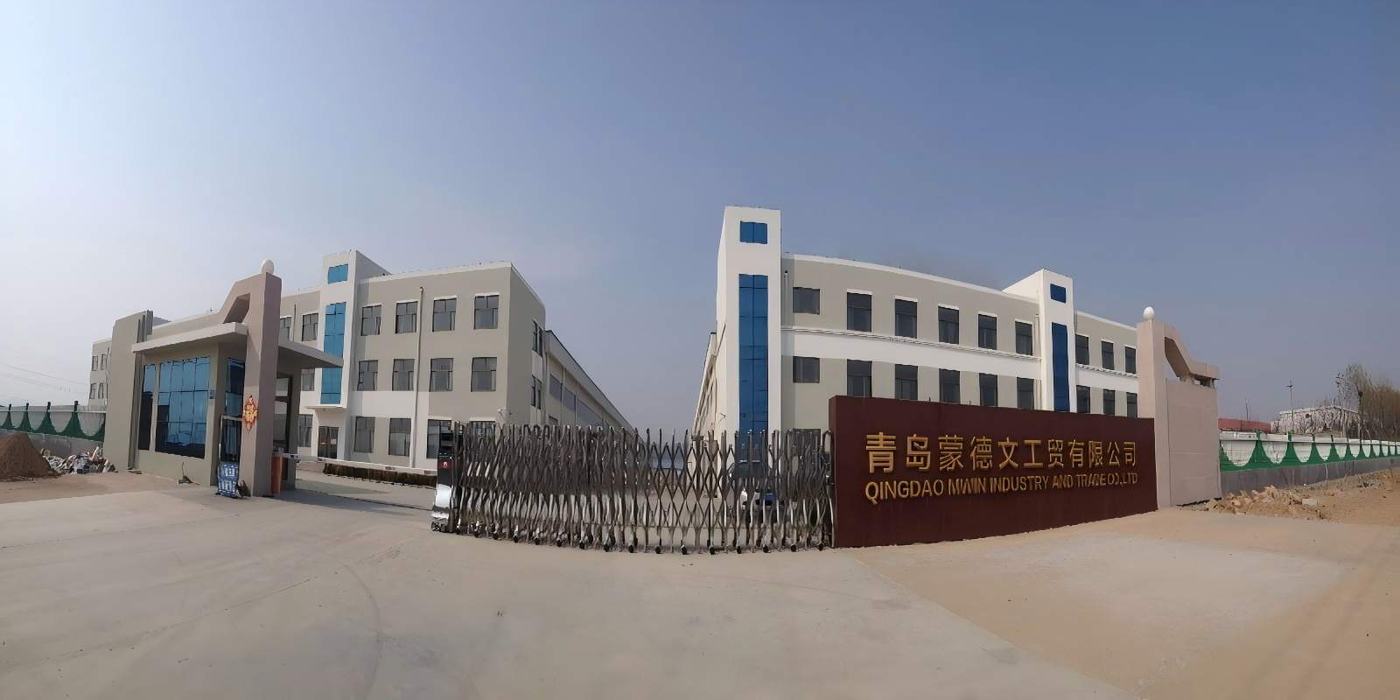
Qingdao MWin Industry and Trade Co., Ltd. is a professional manufacturer focused on heavy-duty rubber conveyor belts for bulk material handling. Founded in 2008 and operating a 58,000 m² production base, we design and produce customized belts for mining, cement plants, power stations, steel mills, aggregate quarries and port bulk handling projects. We strictly follow international standards including ISO and ASTM, offering stable quality, competitive lead time and full technical support for global clients.
Founded in 2008, our manufacturing base covers an area of 58,000 square meters with complete production lines for rubber conveyor belts. We have a professional team including rubber formula R&D engineers, production technicians and QC inspectors.
We focus on heavy industry bulk conveying solutions, deeply understanding harsh working environments such as high temperature, sharp ore impact, heavy abrasion and continuous 24h operation.
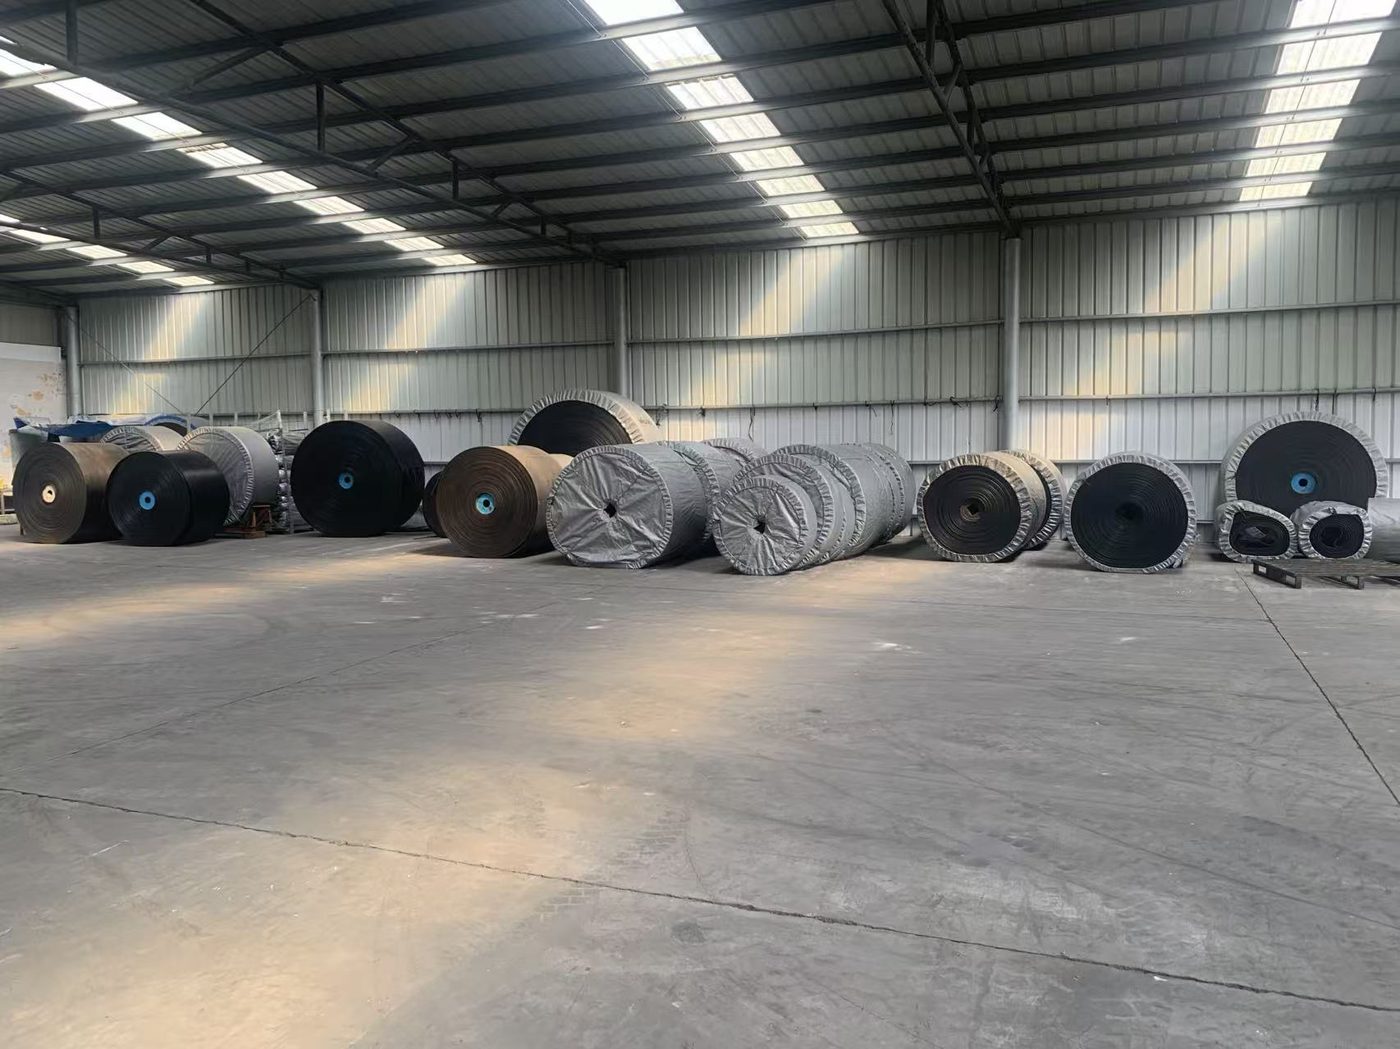
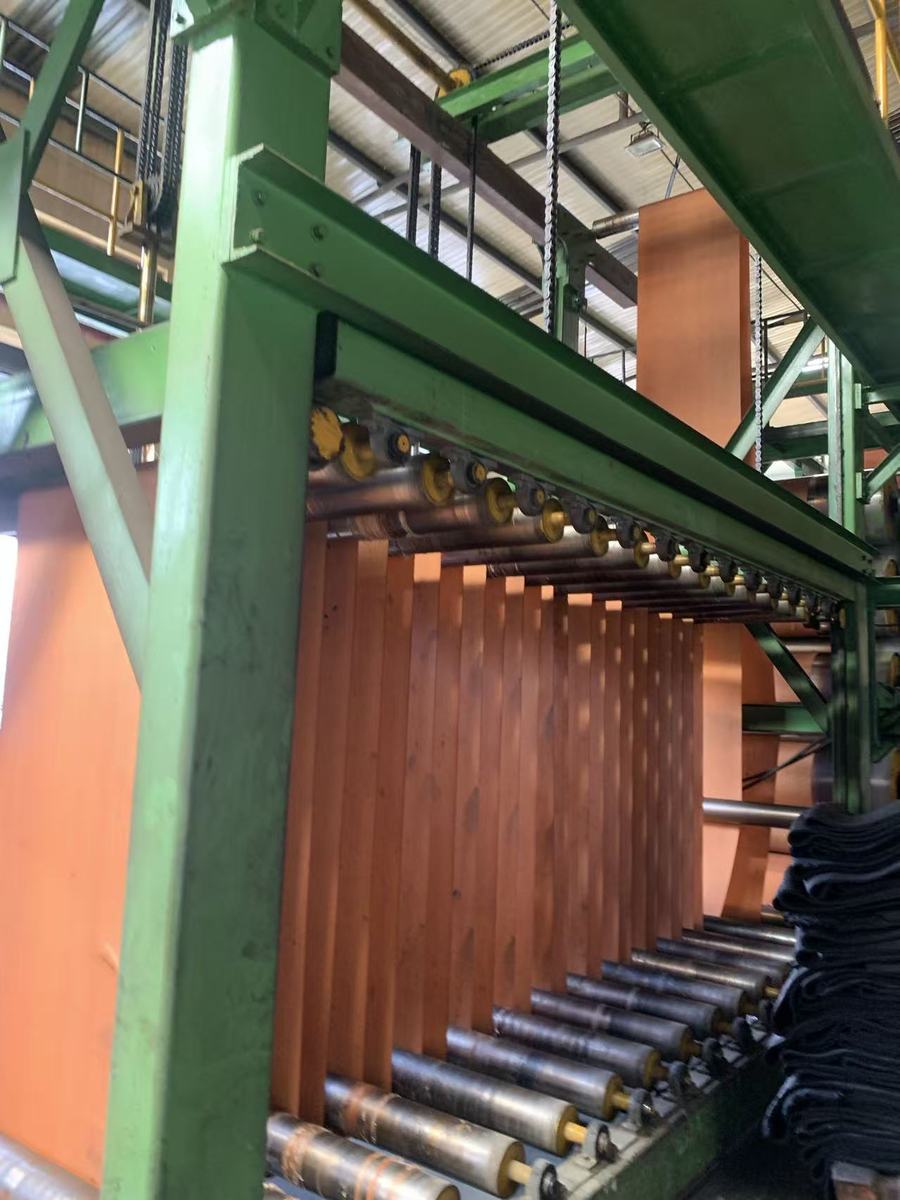
We own full-process production workshops from raw rubber compounding to finished belt inspection and packaging.

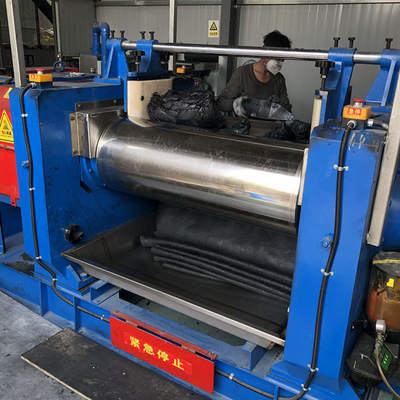
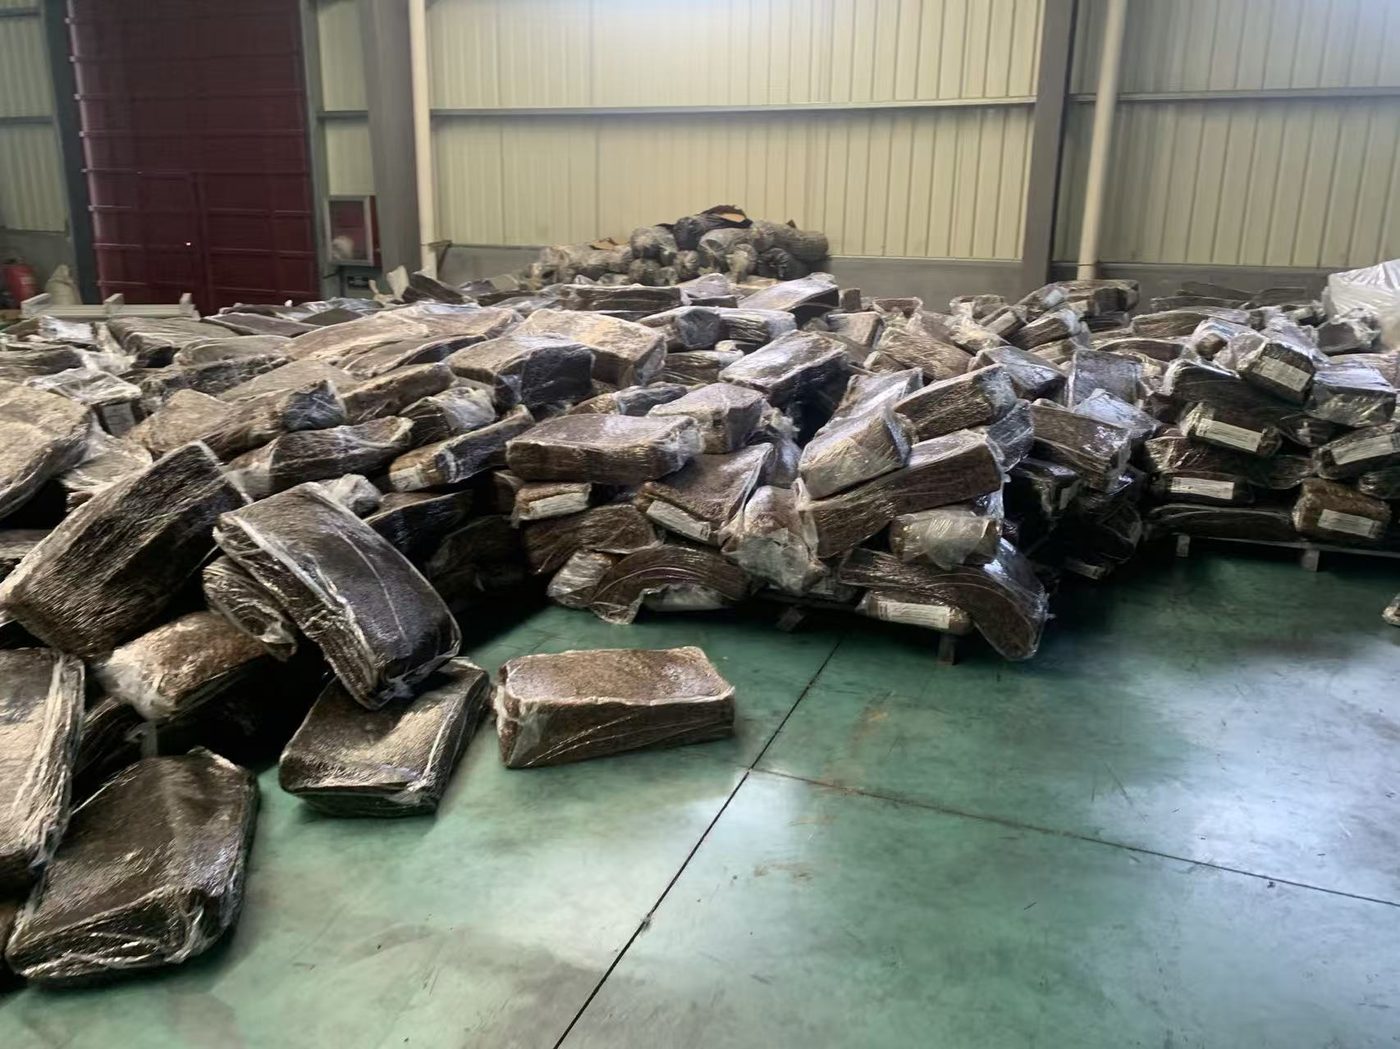
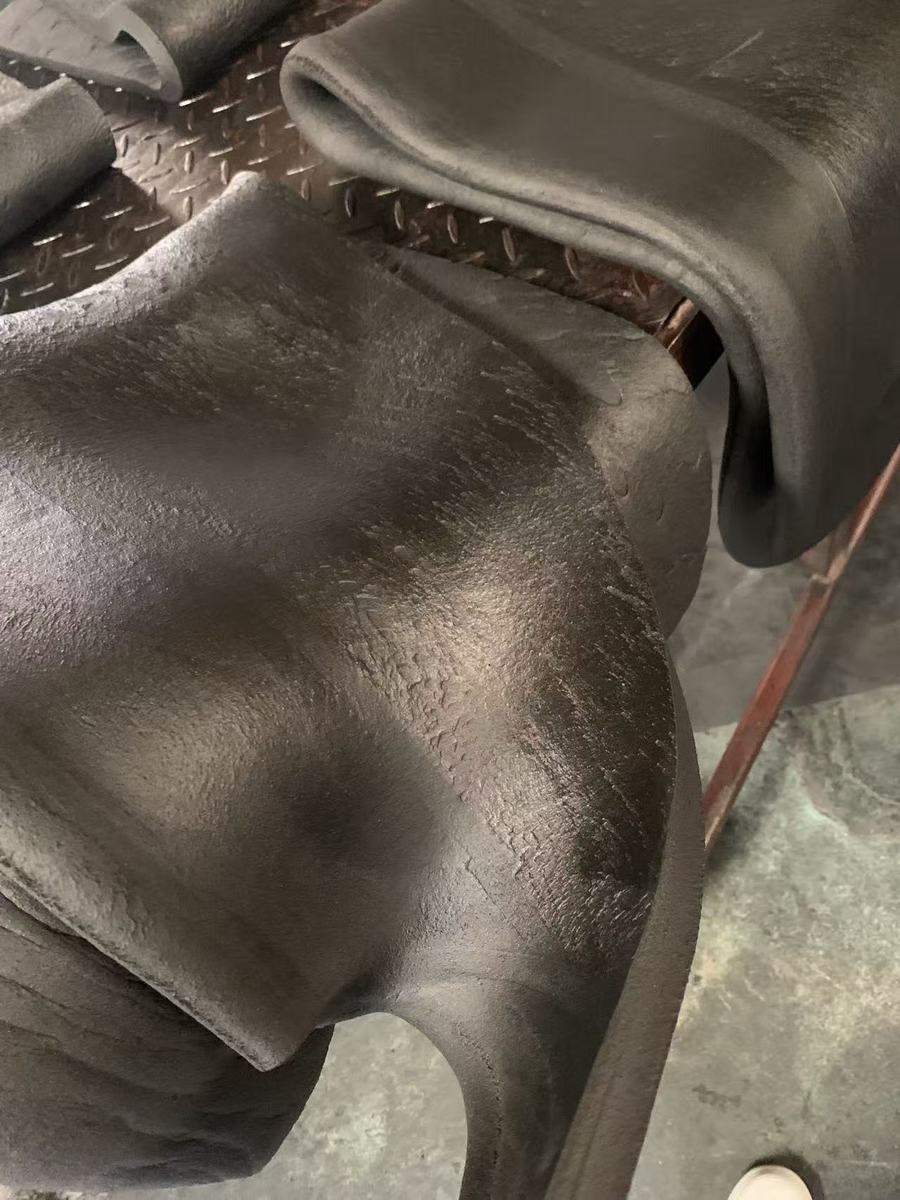
Raw rubber, carbon black, antioxidants and other additives are proportioned and mixed here. Custom rubber formulas are developed here to meet requirements of heat resistance, wear resistance, tear resistance or oil resistance for different site conditions.

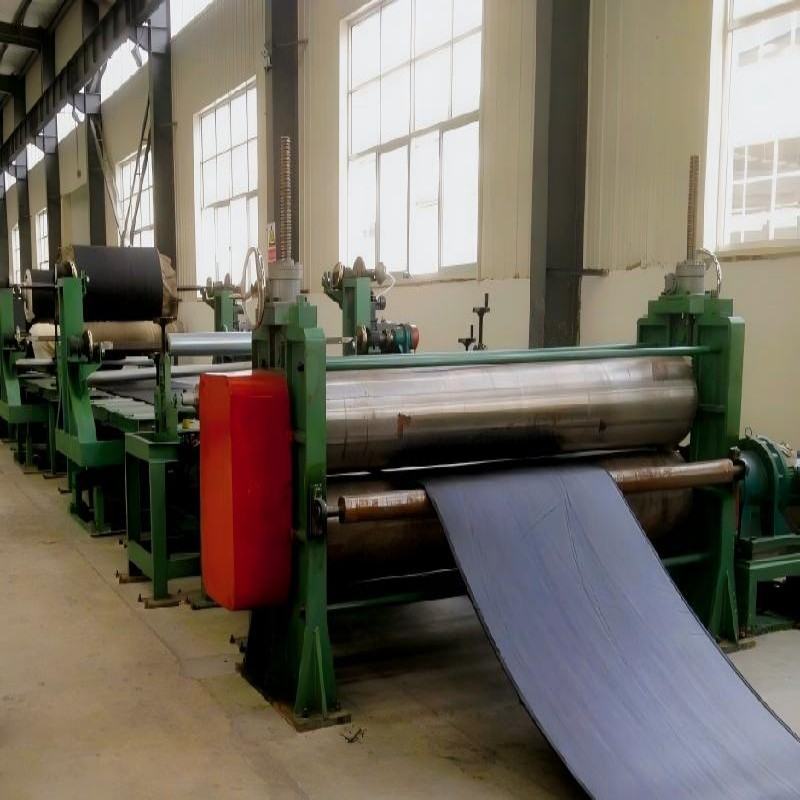
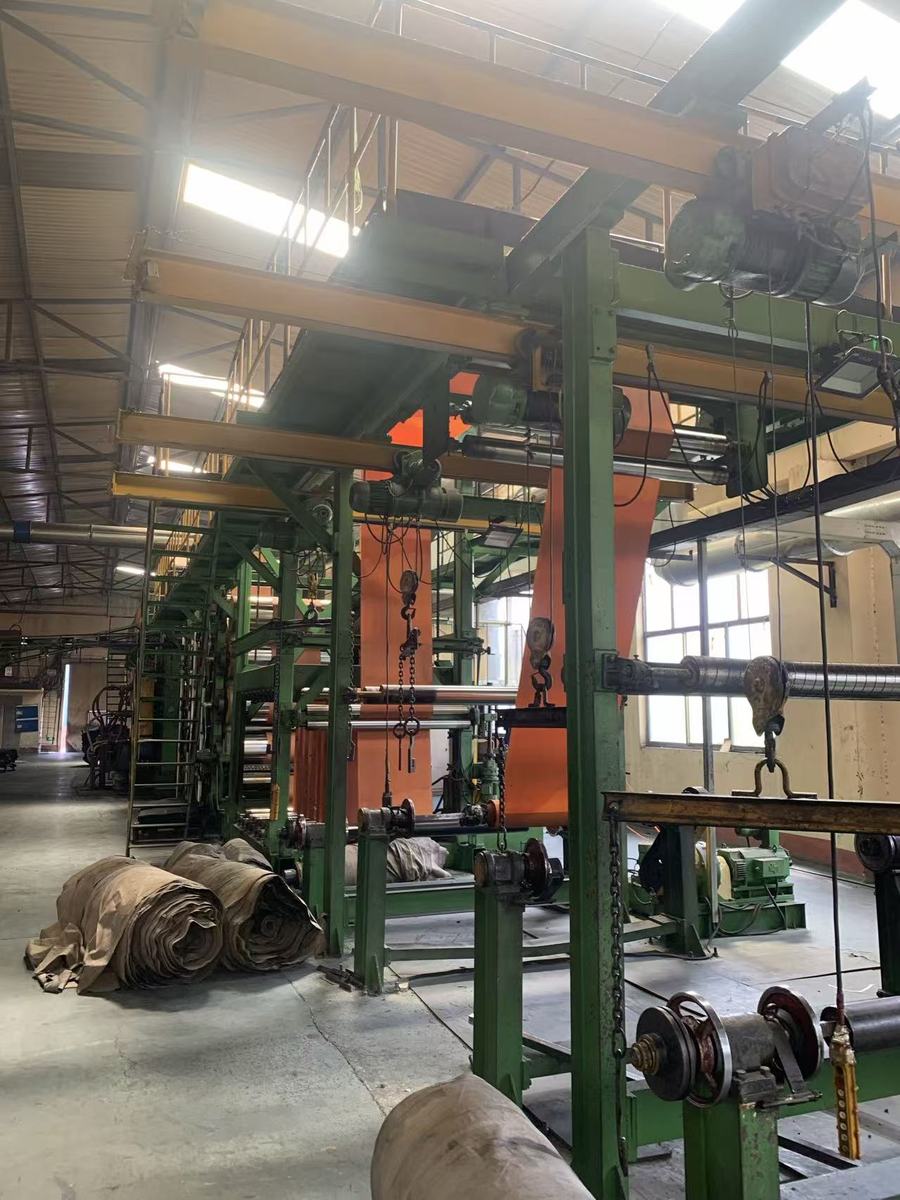
Textile canvas or steel cord materials go through dipping and calendaring. This step ensures strong bonding between carcass and rubber cover, preventing delamination under long-time heavy load.

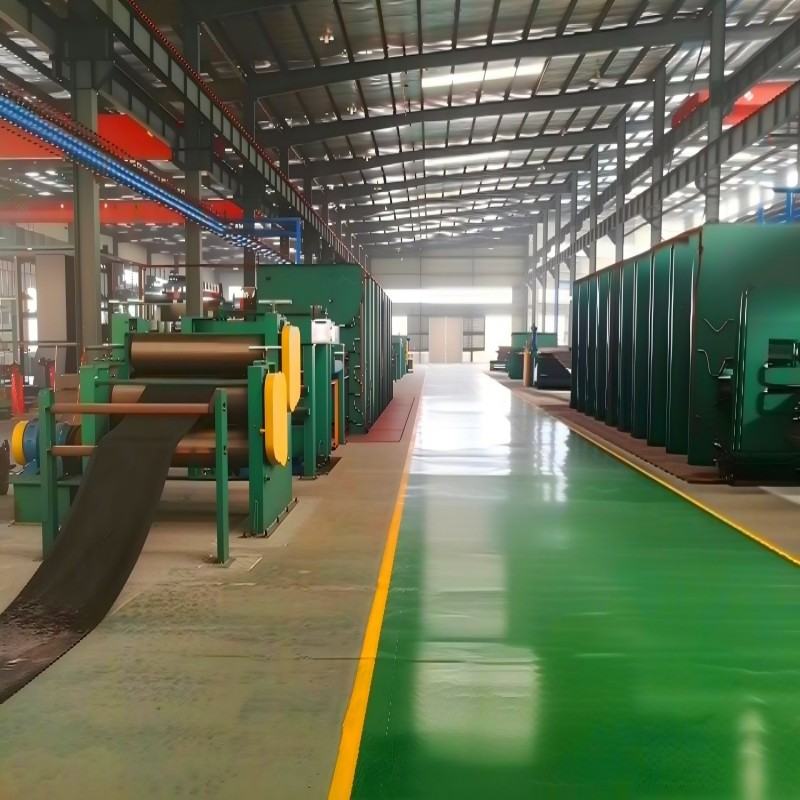
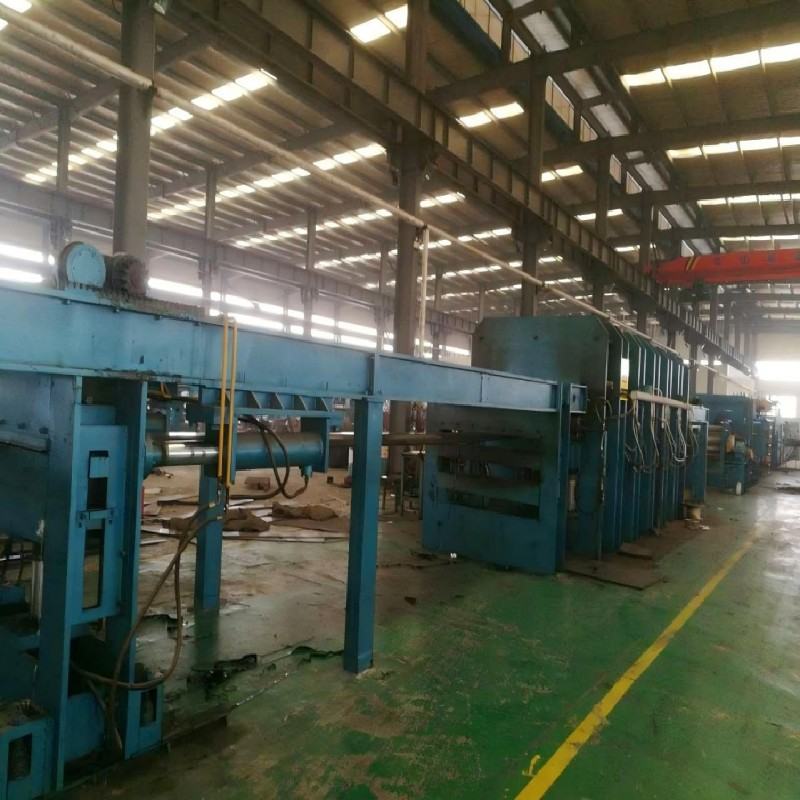
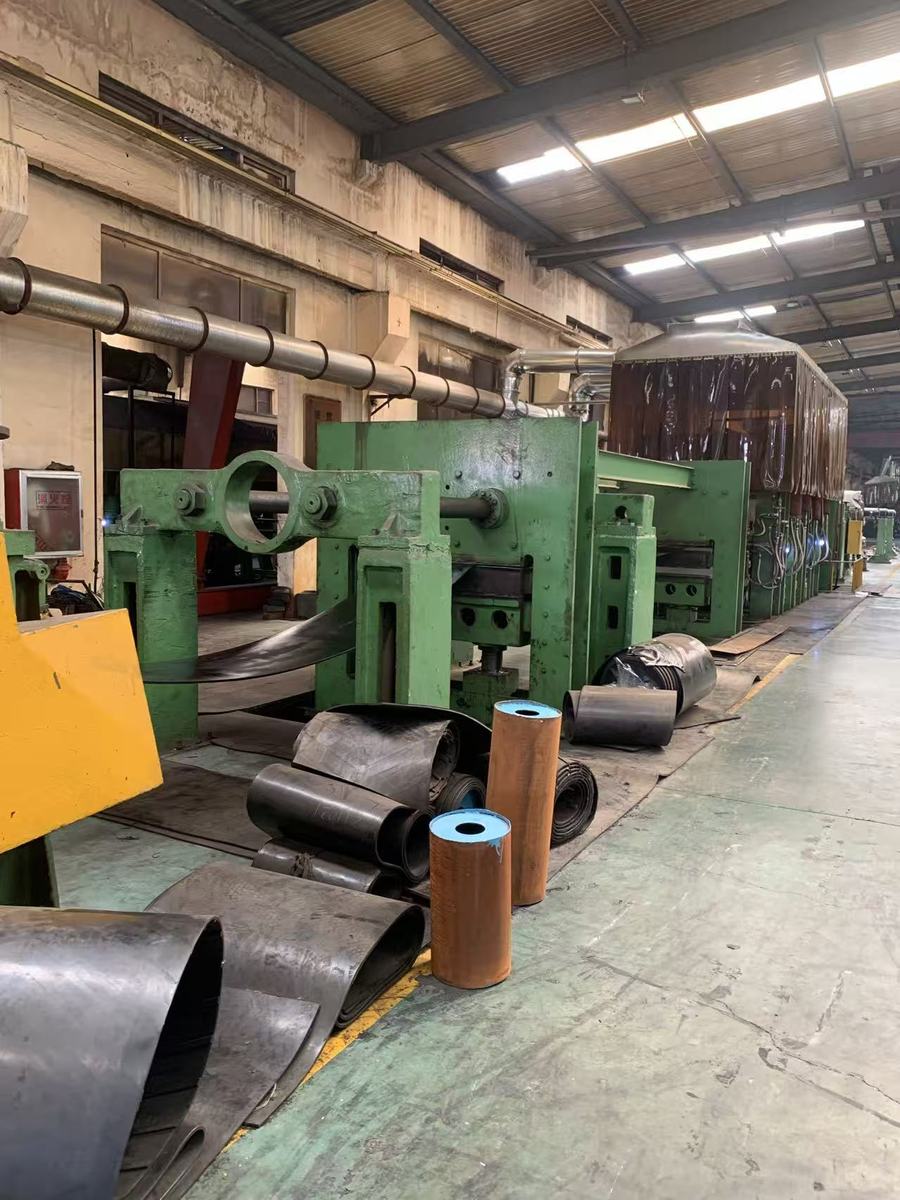
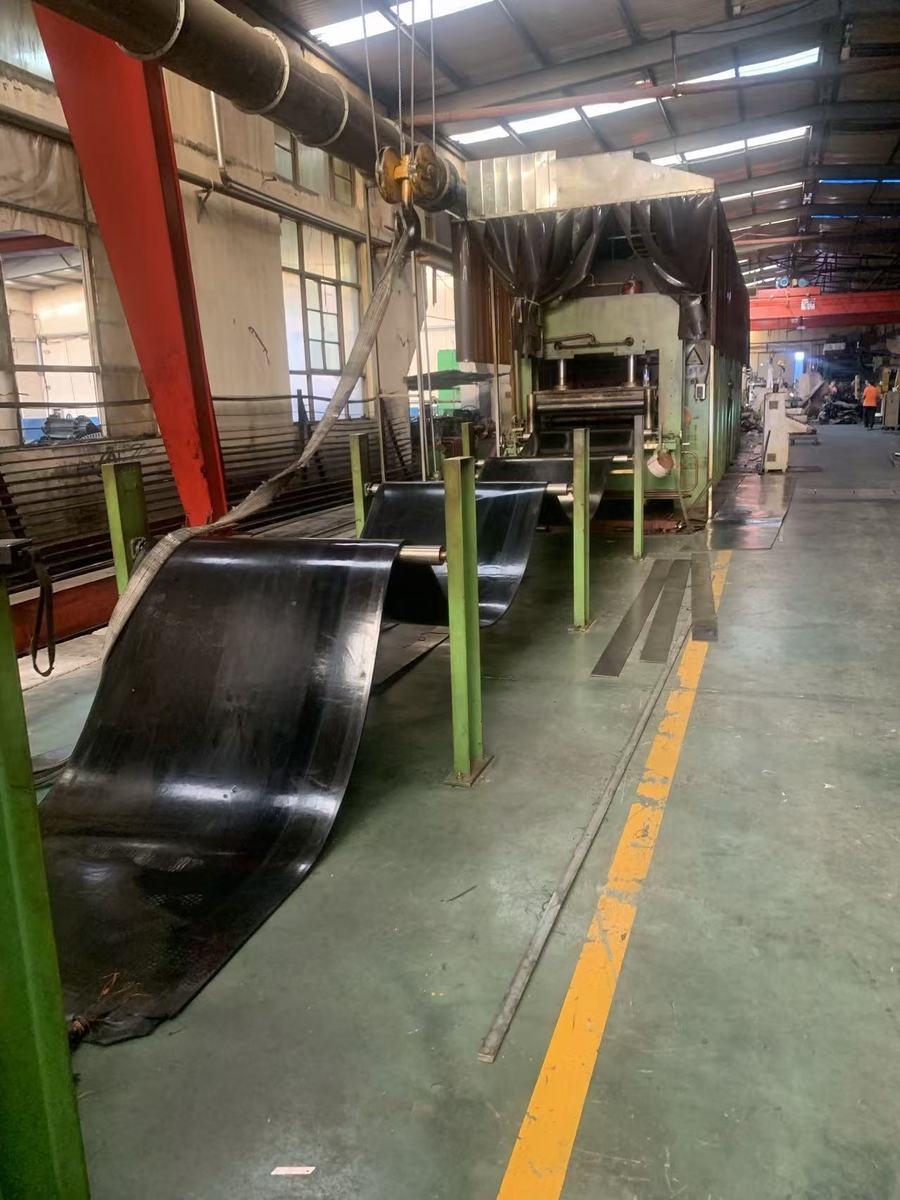
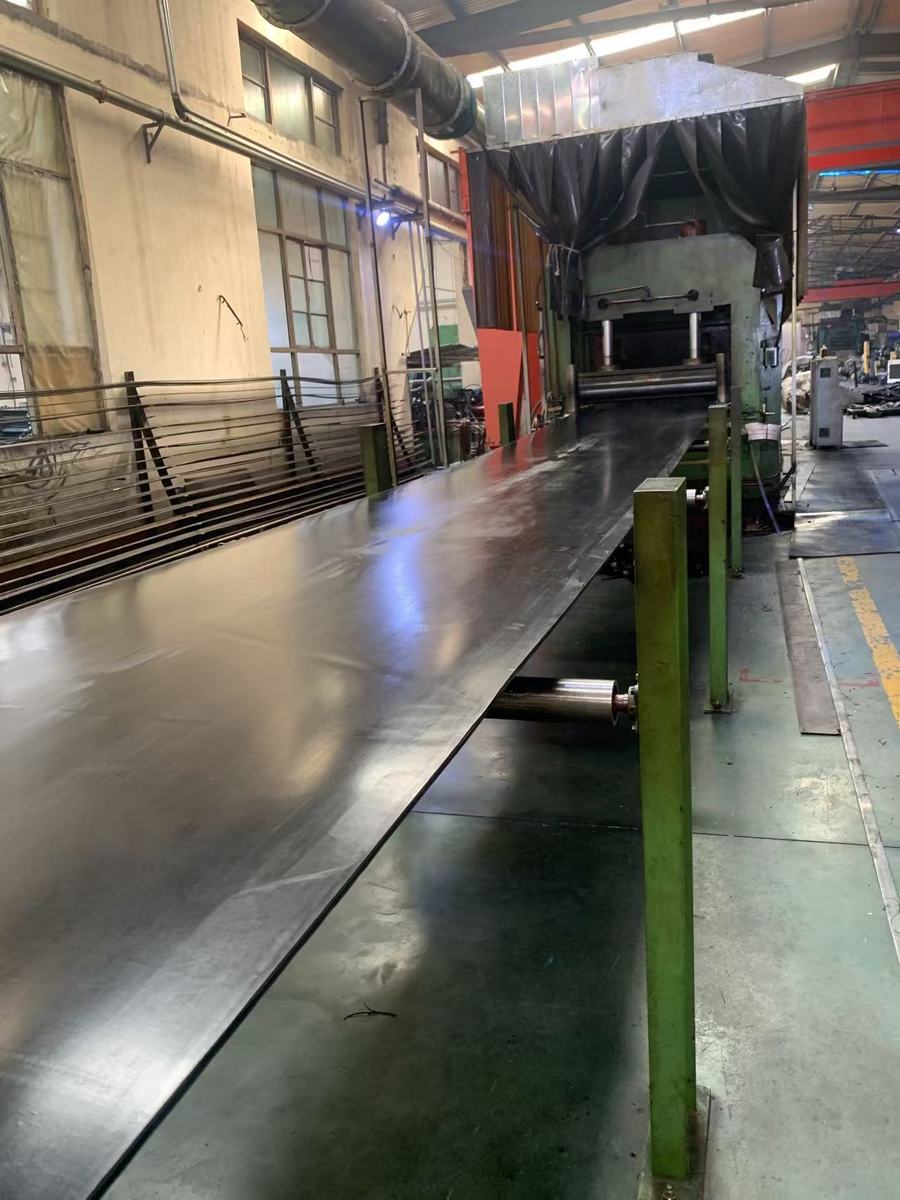
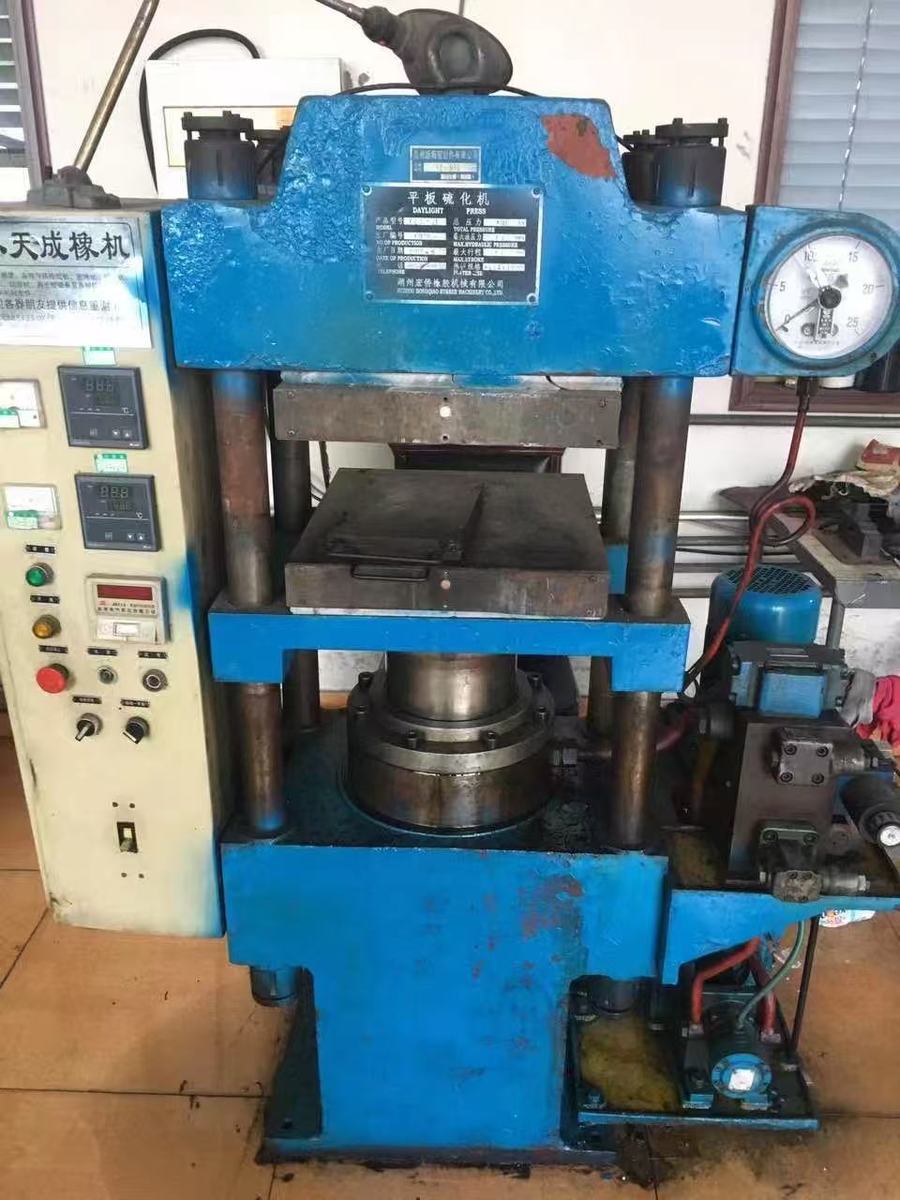
Vulcanization is the core procedure for conveyor belt production. Under controlled temperature and pressure, the rubber forms stable physical properties to resist abrasion, impact and aging. Our continuous vulcanizing equipment guarantees consistent quality for long-length belts.

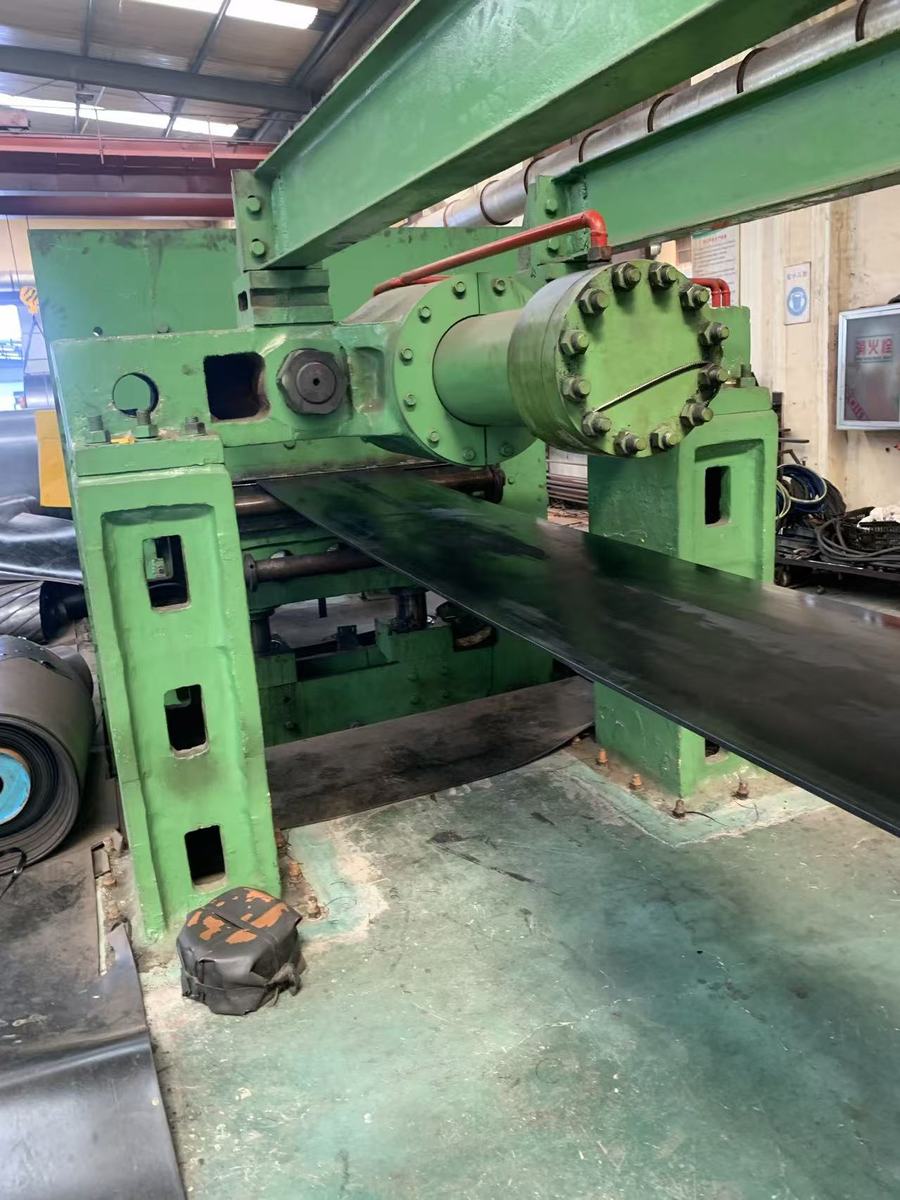
Finished belts are cut into required widths and lengths. Edge trimming, surface cleaning and marking are completed here according to order specifications.

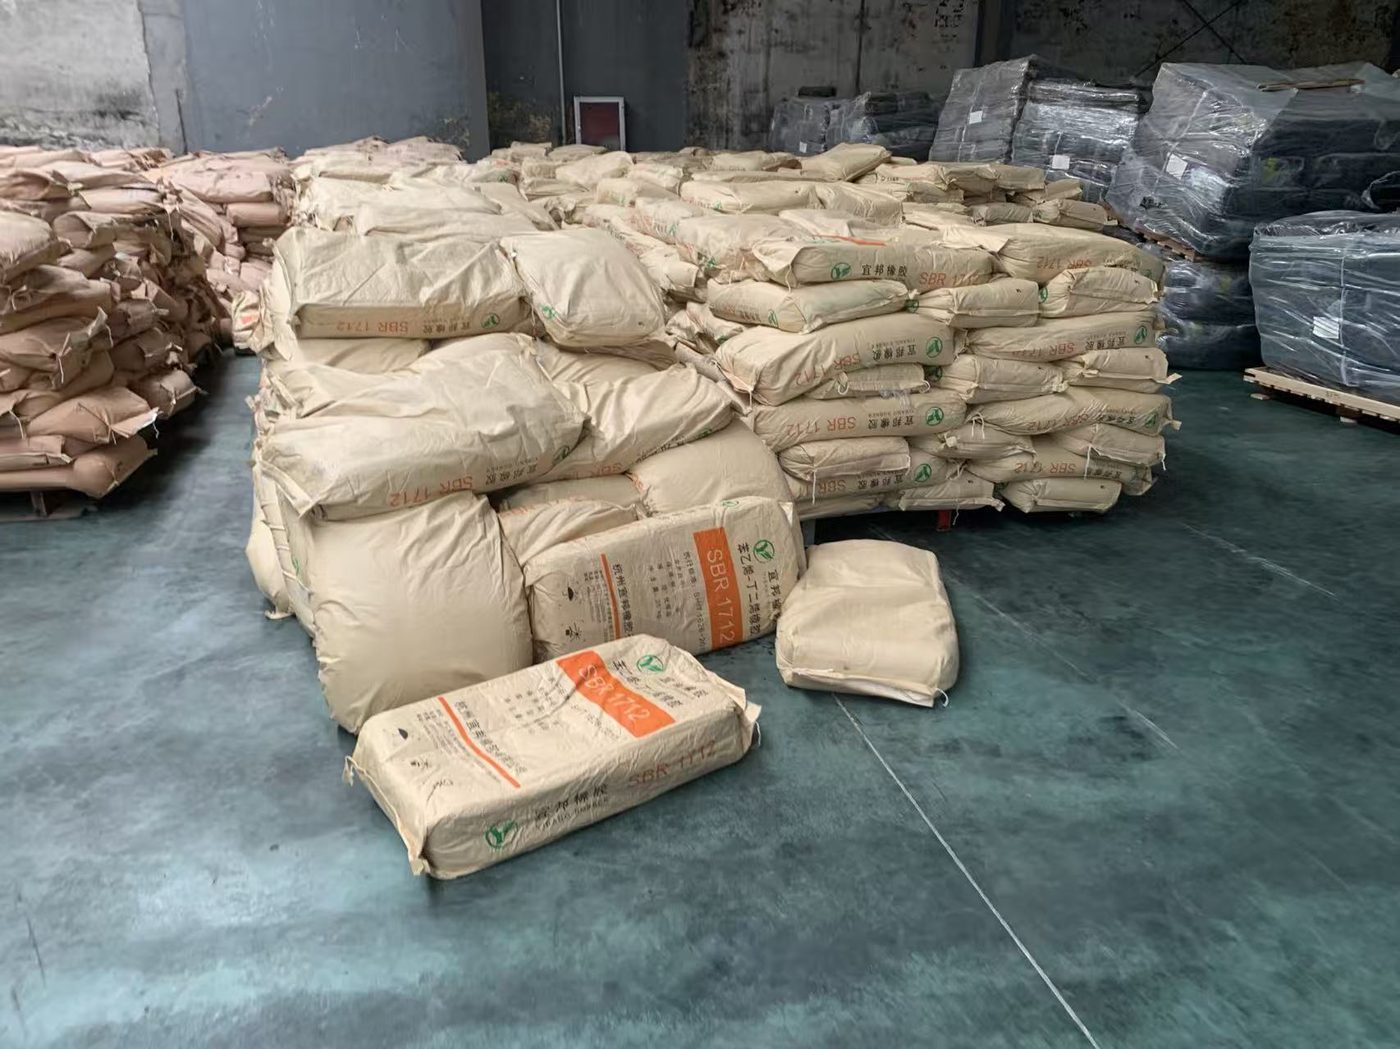
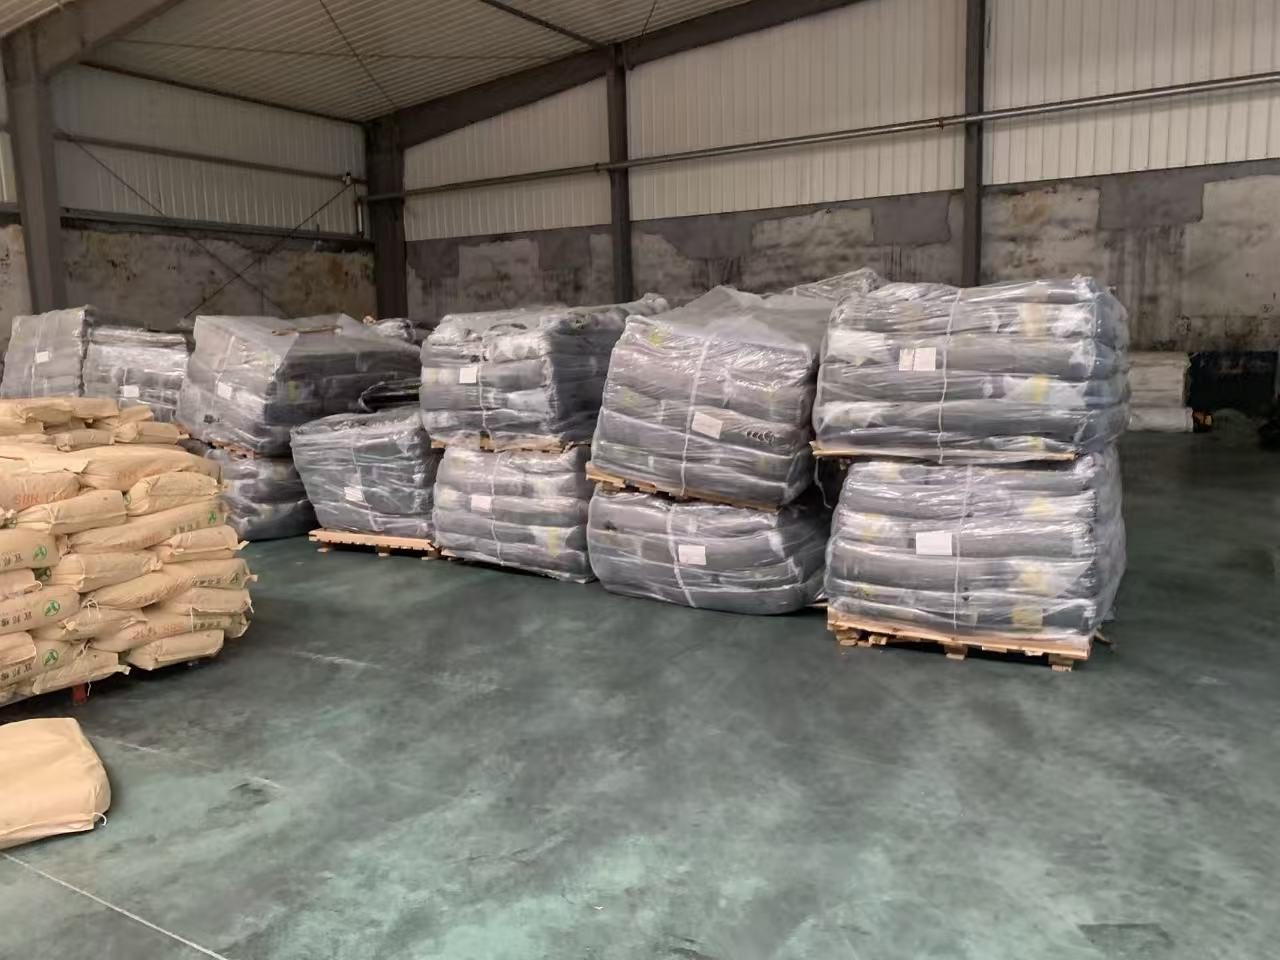
A dedicated warehouse stores raw rubber, SBR, carbon black and fabric carcass in a dry, shaded and well-organized environment. Proper material storage keeps compounds clean and stable, which directly supports consistent belt quality and shorter production lead time.
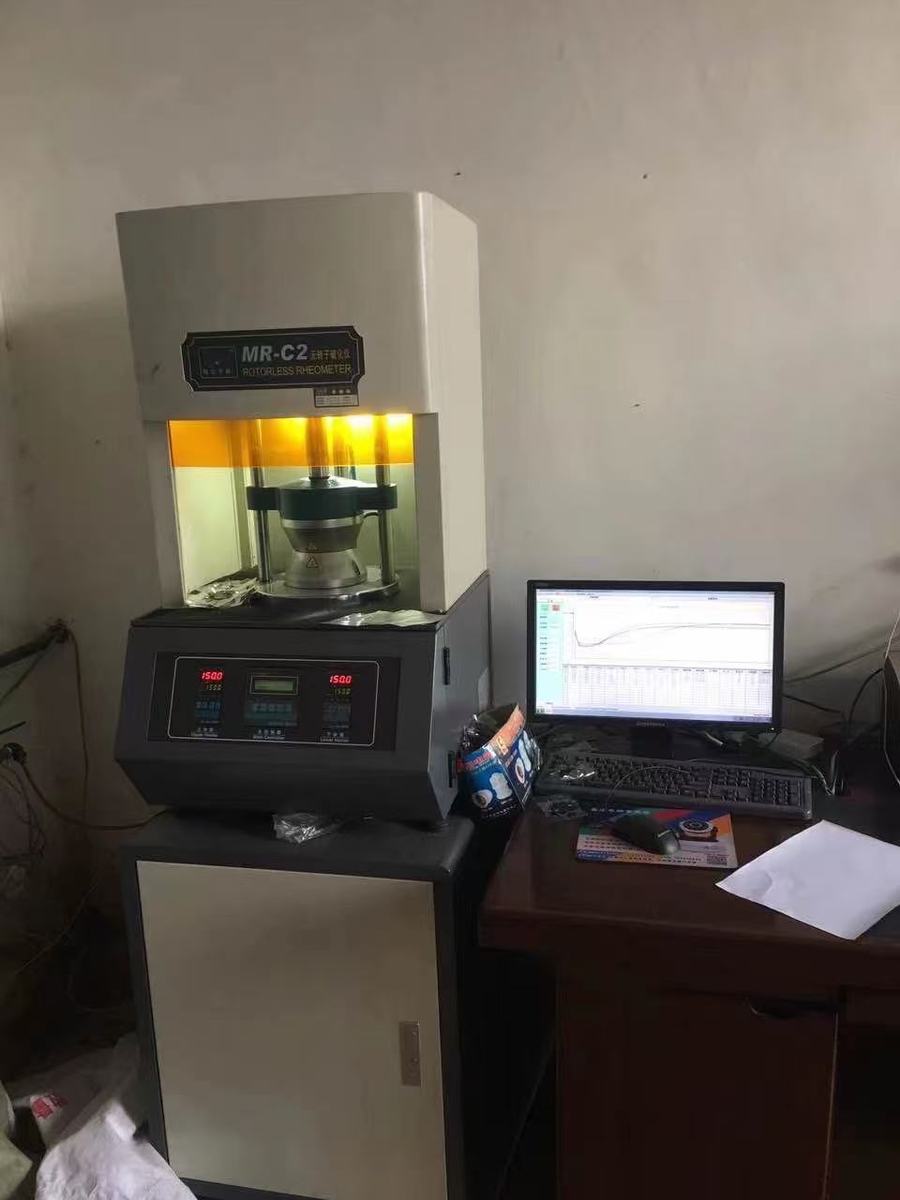
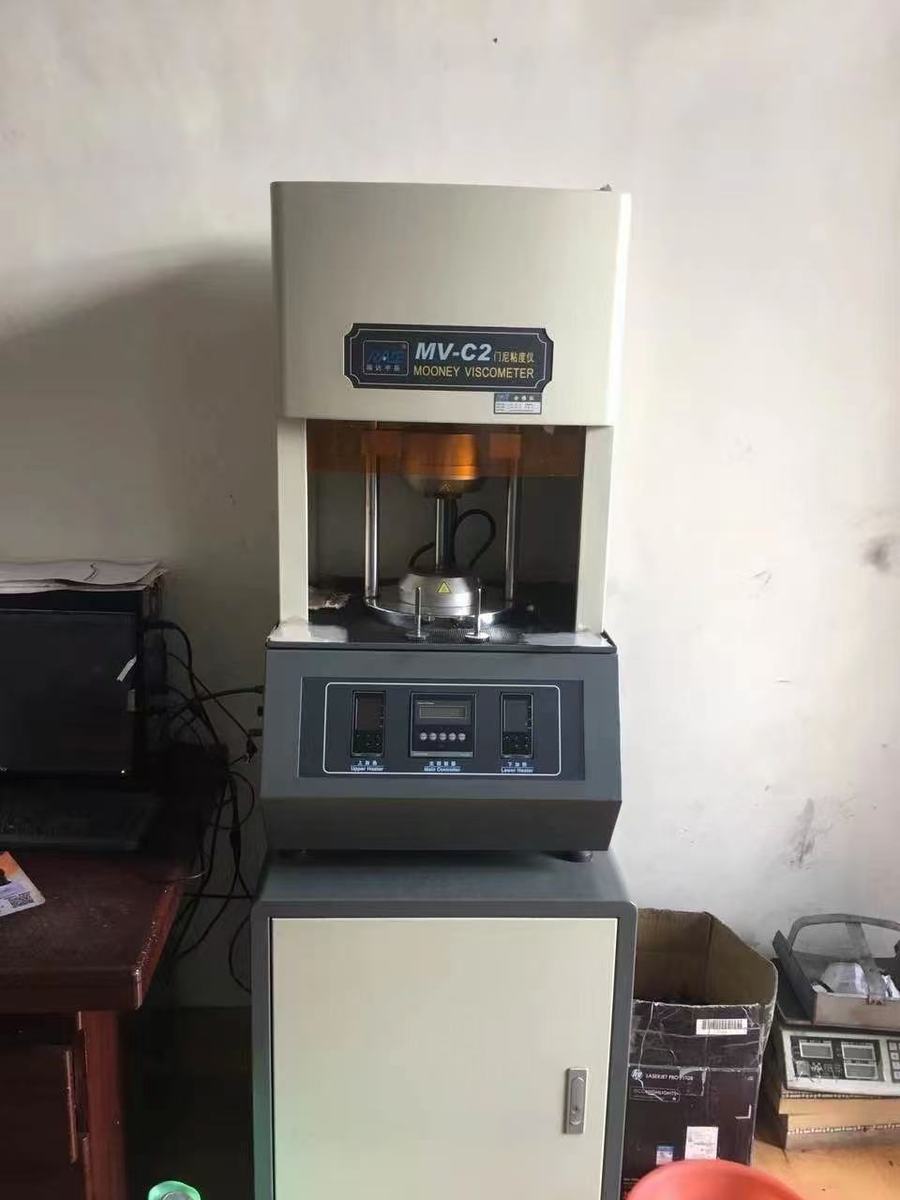
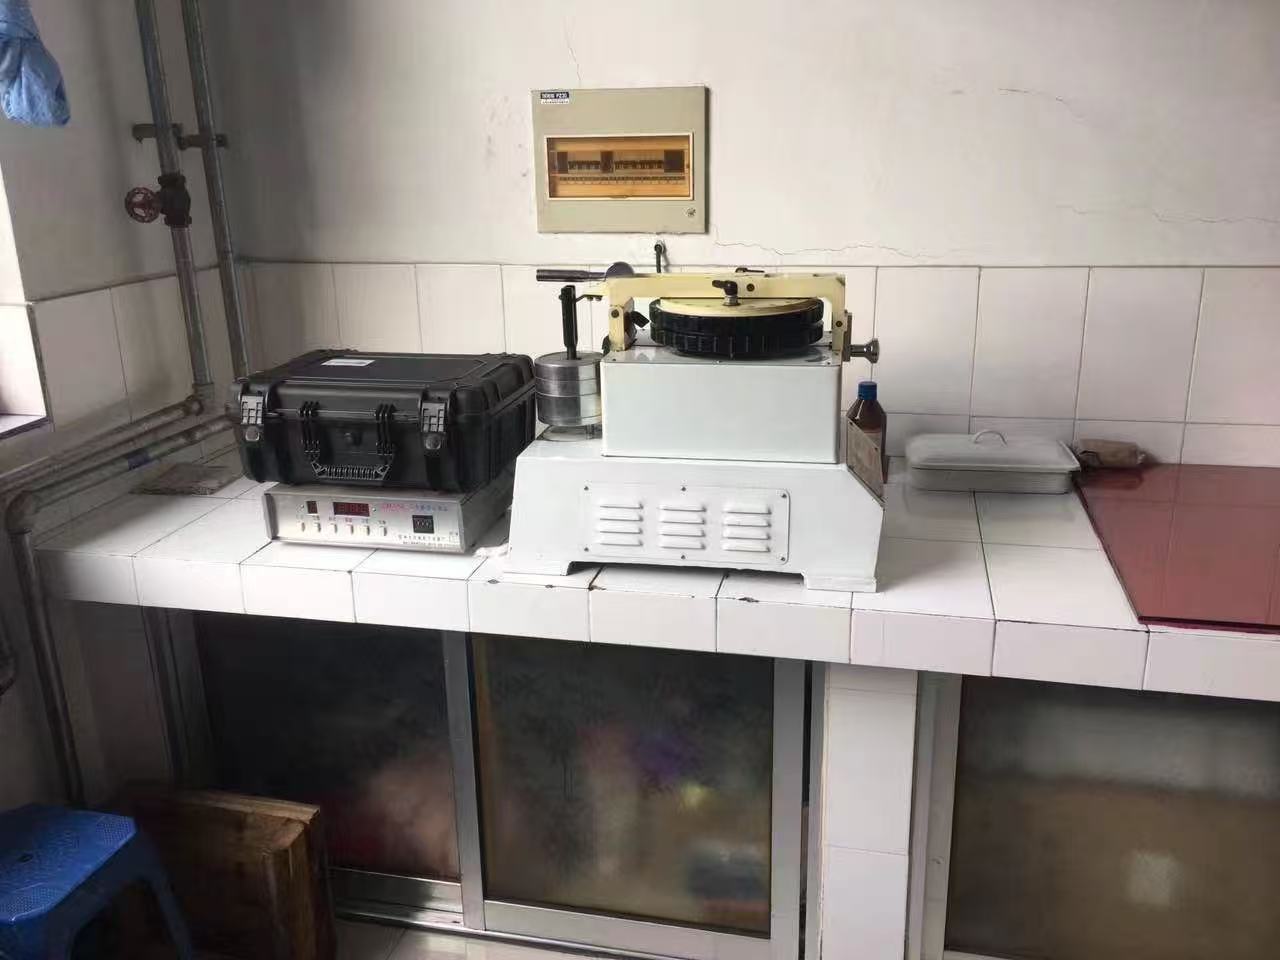
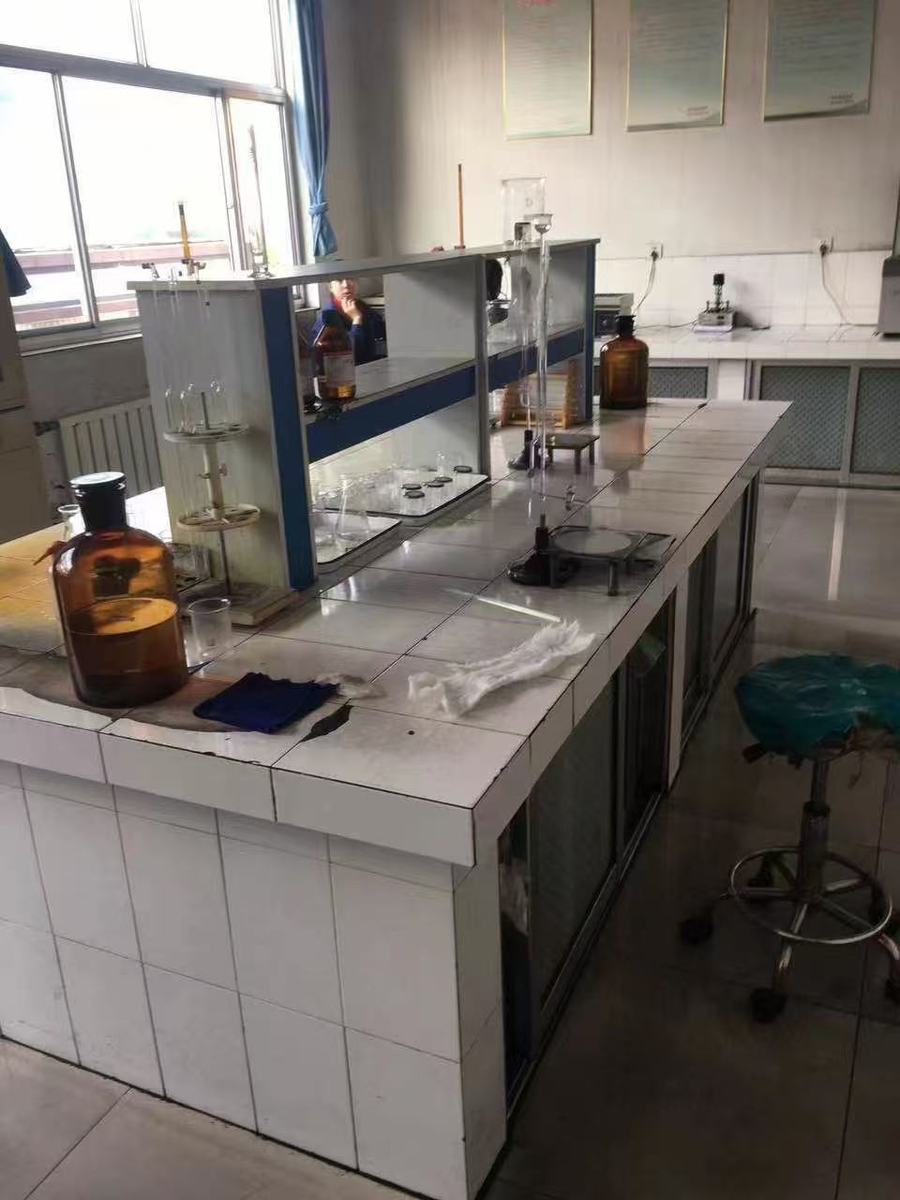
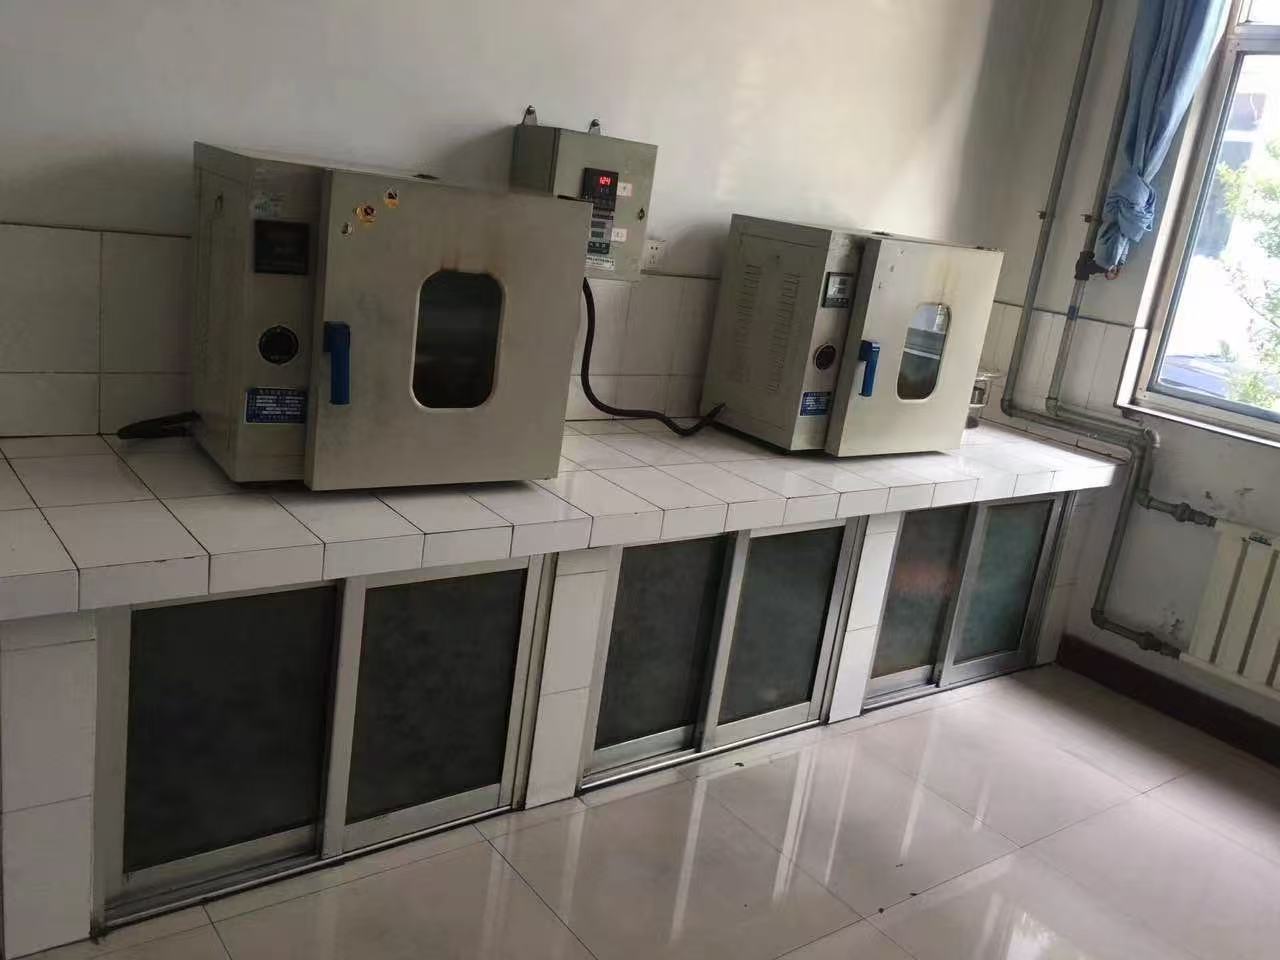
Our factory is equipped with full sets of manufacturing and laboratory testing machines to control quality from raw materials to final products.
Internal mixer for rubber compound mixing.
Calender machine for rubber coating and laminating.
Continuous vulcanizing production line.
Belt slitter and cutting machine.
Tensile strength tester.
Abrasion resistance tester.
Heat aging test chamber.
Tear strength testing machine.
Adhesion strength tester.
Quality is the top priority for heavy-duty conveyor belts, especially for mining and cement plant projects where belt failure may cause costly downtime.
Our QC process runs through the whole production flow:
We can provide test reports according to ASTM or ISO standards. All products can be inspected by third-party organizations such as SGS and BV upon client request.
Certifications: ISO 9001 Quality Management System, SGS test certificates, factory audit support.
We supply conveyor belts for heavy industry bulk material conveying worldwide. Below are our main application fields — each with a full case study.
Lumpy ore and crushed rock transportation for open pit and underground mines.
Sinter, coke and pellet transport for blast furnace.
We accept both small trial orders and large bulk project orders.
Tell us the width, length, strength and material you convey — we will come back with a technical proposal and budget price.
Start WhatsApp Chat